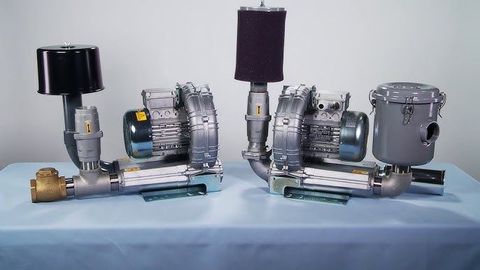
Industrial equipment plays a central role in modern manufacturing, construction, logistics, energy production, agriculture, and many other industries. From machines that move heavy materials to systems that automate production lines, industrial equipment helps businesses produce goods efficiently, safely, and consistently.
As industries continue to adopt automation, smart manufacturing, and energy-efficient technologies, understanding industrial equipment has become increasingly important for business owners, engineers, students, technicians, and anyone interested in industrial operations.
This guide explains what industrial equipment is, why it matters, the major categories, how different equipment works, recent industry developments, maintenance practices, workplace safety, and future trends shaping industrial operations.
What Is Industrial Equipment?
Industrial equipment refers to machines, tools, mechanical systems, and electrical systems used in industrial environments to perform manufacturing, processing, material handling, construction, packaging, testing, and maintenance tasks.
Unlike household or commercial equipment, industrial equipment is designed to operate under demanding conditions for long periods while handling large workloads with precision and reliability.
Industrial equipment may operate manually, semi-automatically, or fully automatically depending on the production process. Many modern machines are integrated with sensors, programmable controllers, and software that monitor performance in real time.
Industrial equipment is found in factories, warehouses, mining sites, power plants, chemical processing facilities, food processing plants, textile industries, pharmaceutical manufacturing, automotive production, and infrastructure projects.
Why Industrial Equipment Is Important Today
Industrial equipment improves productivity by reducing manual effort and increasing production speed. Machines can perform repetitive tasks with greater consistency than manual labor, helping industries maintain product quality while reducing production errors.
Modern equipment also supports workplace safety by minimizing employee exposure to hazardous environments, heavy lifting, extreme temperatures, and repetitive physical work.
Industries increasingly depend on equipment that consumes less energy, reduces waste, improves resource utilization, and supports environmental sustainability. As manufacturing becomes more digital, industrial equipment is evolving into intelligent systems capable of collecting operational data and predicting maintenance needs.
For businesses, reliable equipment contributes to lower downtime, better operational efficiency, improved production planning, and long-term operational stability.
Major Types of Industrial Equipment
Industrial equipment includes a wide range of machines designed for different industrial functions. Each category serves a specific purpose within production and operational workflows.
Material Handling Equipment
Material handling equipment is used to transport, lift, store, and organize materials within industrial facilities. This equipment reduces manual handling and improves workflow efficiency across warehouses and production plants.
Examples include forklifts, conveyors, pallet trucks, cranes, hoists, automated guided vehicles, and storage systems.
These systems are commonly used in logistics, manufacturing, ports, warehouses, and distribution centers.
Manufacturing Equipment
Manufacturing equipment converts raw materials into finished products through machining, forming, cutting, assembling, or processing operations.
Examples include CNC milling machines, CNC lathes, injection molding machines, industrial presses, welding machines, cutting machines, laser cutters, and industrial robots.
This equipment is essential in automotive, aerospace, electronics, metal fabrication, plastics, and precision engineering industries.
Processing Equipment
Processing equipment changes the physical or chemical properties of materials during production.
Examples include mixers, reactors, pumps, compressors, filtration systems, heat exchangers, boilers, dryers, and industrial ovens.
These systems are widely used in food processing, pharmaceuticals, chemicals, oil and gas, textiles, and water treatment industries.
Packaging Equipment
Packaging equipment prepares finished products for storage, transportation, and retail distribution.
Examples include filling machines, labeling machines, sealing machines, wrapping systems, palletizers, bottling equipment, and carton packaging machines.
Packaging systems help improve product consistency, hygiene, and production speed.
Power Generation and Utility Equipment
Industrial facilities require equipment that generates, distributes, and manages energy and utilities.
Examples include generators, transformers, electrical distribution panels, industrial batteries, compressors, chillers, cooling towers, and air handling systems.
Utility equipment supports uninterrupted industrial operations while maintaining power quality and environmental control.
How Industrial Equipment Works
Industrial equipment operates through a combination of mechanical, hydraulic, pneumatic, electrical, and electronic systems.
Mechanical systems use gears, shafts, belts, bearings, motors, and rotating components to transfer motion and force. Hydraulic systems use pressurized fluids to generate powerful movement for lifting, pressing, or moving heavy loads.
Pneumatic systems use compressed air to operate cylinders, valves, and automation components in assembly lines and packaging systems.
Electrical systems provide power to motors, drives, sensors, controllers, and safety devices. Modern equipment often includes programmable logic controllers, variable frequency drives, and industrial sensors that automate machine operations.
Many machines now communicate with factory software through industrial communication protocols, allowing operators to monitor performance, production output, temperature, vibration, pressure, and energy consumption from centralized control systems.
Common Applications Across Industries
Industrial equipment supports a wide variety of industries, each with specialized operational requirements.
| Industry | Equipment Applications |
|---|---|
| Manufacturing | Machining, assembly, welding, robotics, packaging |
| Construction | Earthmoving, lifting, concrete mixing, drilling, excavation |
| Food Processing | Mixing, cooking, filling, packaging, refrigeration |
| Pharmaceuticals | Sterile processing, filling, inspection, packaging |
| Oil and Gas | Pumps, compressors, valves, pipelines, processing equipment |
| Textile Industry | Spinning, weaving, dyeing, finishing, recycling systems |
| Mining | Crushing, conveying, drilling, material transport |
| Renewable Energy | Solar manufacturing, wind turbine components, battery production |
Each industry selects equipment based on production volume, material characteristics, operating conditions, and regulatory requirements.
Benefits of Modern Industrial Equipment
Industrial equipment provides significant operational advantages when properly selected and maintained.
Modern machines improve production speed while maintaining consistent product quality. Automated systems reduce manual intervention and improve process accuracy across repetitive manufacturing operations.
Equipment also helps reduce material waste through precise measurement, controlled processing, and automated quality inspection. Advanced sensors identify process deviations before they become major production issues.
Energy-efficient motors, drives, compressors, and heating systems help industries reduce electricity consumption and improve sustainability goals.
Another major benefit is scalability. Industrial facilities can expand production capacity by integrating additional machines or upgrading automation systems without completely redesigning production lines.
Digital monitoring systems provide operational visibility, allowing maintenance teams to identify inefficiencies and schedule repairs before unexpected equipment failures occur.
Choosing the Right Industrial Equipment
Selecting industrial equipment depends on operational needs rather than simply choosing the largest or newest machine.
Production capacity is one of the first considerations. Equipment should match expected production volume without creating unnecessary operating costs.
Material compatibility is equally important because different materials require different processing methods, temperatures, pressures, and handling systems.
Available factory space influences equipment size, installation layout, maintenance access, and future expansion possibilities.
Energy consumption, automation level, maintenance requirements, safety features, and compatibility with existing production systems also play important roles during equipment selection.
Industries often evaluate equipment based on reliability, operational efficiency, serviceability, and long-term productivity instead of focusing only on initial investment considerations.
Maintenance and Equipment Reliability
Maintenance is essential for keeping industrial equipment operating safely and efficiently throughout its service life.
Preventive maintenance involves scheduled inspections, lubrication, cleaning, alignment checks, filter replacement, and calibration before equipment develops faults.
Predictive maintenance uses sensors to monitor vibration, temperature, pressure, oil quality, and electrical performance. This approach helps identify early signs of wear before breakdowns occur.
Corrective maintenance addresses equipment failures after faults are detected. While necessary in some situations, relying only on corrective maintenance can increase downtime and production interruptions.
Maintenance documentation helps organizations track service history, replacement schedules, inspection records, and recurring operational issues.
Well-maintained equipment typically experiences fewer unexpected shutdowns, better operational efficiency, longer component life, and improved workplace safety.
Industrial Safety and Equipment Standards
Industrial equipment must operate within established workplace safety practices and engineering standards.
Machine guarding protects workers from moving parts, rotating shafts, cutting tools, and hazardous operating zones.
Emergency stop systems allow machines to shut down immediately during abnormal operating conditions or emergencies.
Lockout and tagout procedures ensure equipment is safely isolated before maintenance or repairs begin, reducing accidental equipment startup.
Personal protective equipment remains an important part of industrial safety, particularly when operating machinery involving heat, chemicals, noise, dust, or heavy materials.
Routine inspections help identify damaged cables, hydraulic leaks, worn components, overheating motors, and safety device failures before they become operational hazards.
A strong safety culture combines equipment design, operator training, maintenance procedures, and workplace awareness.
Recent Updates in Industrial Equipment (2025–2026)
Industrial equipment continues evolving as manufacturers adopt digital technologies and sustainability initiatives.
Smart factories increasingly integrate Industrial Internet of Things sensors into machines for real-time monitoring and predictive maintenance. Connected equipment provides continuous operational insights through centralized dashboards.
Artificial intelligence is being incorporated into inspection systems, robotics, and machine monitoring to identify defects, optimize production schedules, and improve maintenance planning.
Collaborative robots have become more common in manufacturing environments where humans and robots work together during assembly, packaging, inspection, and material handling tasks.
Energy-efficient equipment has become a priority as industries seek lower energy consumption and reduced environmental impact through efficient motors, variable speed drives, heat recovery systems, and optimized compressors.
Digital twins are gaining attention as manufacturers create virtual models of equipment to simulate performance, identify bottlenecks, and improve operational planning before physical changes are implemented.
Remote equipment monitoring is also expanding, allowing maintenance teams to monitor industrial assets across multiple facilities from centralized operational centers.
Sustainability and Energy Efficiency in Industrial Equipment
Sustainability has become an important consideration across industrial operations.
Modern equipment is designed to reduce electricity consumption, minimize emissions, improve water efficiency, and reduce material waste during production.
Variable frequency drives adjust motor speed according to production demand, reducing unnecessary energy use.
High-efficiency compressors and pumps optimize airflow and fluid movement while consuming less power.
Industrial filtration and recycling systems help recover water, chemicals, and process materials for reuse, supporting circular manufacturing practices.
Automation also contributes to sustainability by improving process precision and reducing defective products that require rework or disposal.
As industries adopt renewable energy and digital manufacturing, equipment increasingly supports environmental performance alongside operational productivity.
Future of Industrial Equipment
The future of industrial equipment is closely connected to automation, artificial intelligence, connectivity, and sustainability.
Machines are becoming more intelligent through embedded sensors, edge computing, and cloud-connected monitoring systems. Equipment will increasingly communicate with other machines to optimize production without constant manual intervention.
Autonomous mobile robots are expected to expand material transport capabilities inside warehouses and manufacturing facilities. AI-powered inspection systems will continue improving quality control through computer vision technologies.
Additive manufacturing equipment will complement traditional manufacturing methods in selected industries requiring customized or low-volume production.
Cybersecurity is becoming increasingly important as connected industrial equipment exchanges operational data across factory networks.
The next generation of industrial equipment is expected to combine efficiency, flexibility, safety, predictive maintenance, and environmental responsibility into integrated manufacturing ecosystems.
Conclusion
Industrial equipment forms the foundation of modern industrial production across manufacturing, construction, logistics, energy, agriculture, pharmaceuticals, food processing, and many other sectors. These machines help industries improve productivity, maintain consistent quality, reduce manual effort, and operate more safely under demanding conditions.
As technology advances, industrial equipment is evolving beyond traditional mechanical machines into intelligent, connected systems capable of monitoring performance, predicting maintenance needs, and supporting data-driven decision-making. Energy efficiency, automation, and sustainability are becoming standard considerations in equipment design and industrial operations.
Understanding the different types of industrial equipment, their functions, applications, maintenance practices, and emerging technologies helps businesses and professionals make informed operational decisions while preparing for the future of smart manufacturing and modern industrial infrastructure.