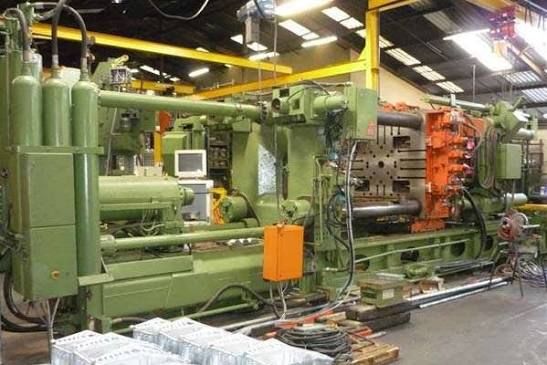
Industrial die casting machines are specialized manufacturing systems used to produce metal components by forcing molten metal.
They are widely used for producing complex components with consistent dimensions, smooth surfaces, and repeatable production characteristics.
Modern die casting equipment combines hydraulic or electric drive systems, precision dies, automated metal handling, process controls, and inspection technologies. Machine selection depends on alloy type, component geometry, casting size, production volume, injection pressure, and required dimensional accuracy.
What Are Industrial Die Casting Machines?
An industrial die casting machine is equipment designed to inject molten metal into a reusable metal die at controlled speed and pressure. After the metal solidifies, the casting is removed and the die is prepared for the next cycle.
The process is particularly suitable for non-ferrous alloys such as:
- Aluminum
- Zinc
- Magnesium
- Copper-based alloys
Die casting can produce components with thin walls, complex shapes, ribs, bosses, holes, and other detailed features.
How Do Die Casting Machines Work?
A typical die casting cycle consists of several stages.
1. Die Preparation
The two halves of the die are cleaned, inspected, and treated with an appropriate release agent. The die is then closed and locked using the machine's clamping system.
2. Metal Melting
The selected alloy is heated in a furnace until it reaches the required molten condition. Temperature control is important because excessive or insufficient temperature can affect filling and casting quality.
3. Metal Injection
Molten metal enters the shot sleeve or injection chamber. A piston then forces the metal into the die cavity at controlled velocity and pressure.
4. Die Filling
The molten metal flows through the runner and gate system into the cavity. Injection parameters must be controlled to reduce defects such as incomplete filling, air entrapment, and turbulence.
5. Solidification
The metal cools and solidifies inside the die. Cooling channels within the die help control thermal conditions and cycle time.
6. Die Opening
Once solidification is sufficient, the clamping system opens the die.
7. Ejection
Ejector pins or related mechanisms push the finished casting from the cavity.
8. Trimming and Finishing
Excess material from gates, runners, overflows, and flash is removed. Additional machining or surface finishing may follow depending on component requirements.
Types of Industrial Die Casting Machines
Different machine configurations are designed for different alloys and production conditions.
Hot Chamber Die Casting Machines
Hot chamber machines integrate the injection mechanism closely with the molten metal bath. This configuration is commonly used with alloys that have relatively low melting temperatures and do not significantly attack the injection components.
Zinc and certain other alloys are frequently processed using hot chamber technology.
Cold Chamber Die Casting Machines
Cold chamber machines use a separate melting furnace. A measured quantity of molten metal is transferred into the injection chamber before each shot.
This configuration is commonly used for aluminum and magnesium alloys and is also applicable to certain copper-based alloys.
High Pressure Die Casting Machines
High pressure die casting systems inject molten metal into the die at high velocity and pressure. They are widely used for high-volume production of detailed metal components.
Low Pressure Die Casting Systems
Low pressure systems introduce molten metal into the mold using controlled pressure rather than the high-speed injection approach associated with high pressure die casting.
They can be suitable for components where controlled filling and material integrity are important.
Key Components of a Die Casting Machine
A complete die casting machine contains several mechanical, hydraulic, electrical, and control components.
| Component | Main Function |
|---|---|
| Clamping Unit | Holds the die halves together |
| Injection Unit | Forces molten metal into the die |
| Hydraulic System | Provides controlled machine movement |
| Die | Forms the component geometry |
| Furnace | Melts and maintains alloy temperature |
| Shot Sleeve | Contains molten metal before injection |
| Plunger | Pushes molten metal into the cavity |
| Ejector System | Removes the solidified casting |
| Cooling System | Controls die temperature |
| Control System | Monitors and regulates machine parameters |
The design of these components varies according to machine type, locking force, shot capacity, and automation level.
Die Casting Machine Specifications
Several specifications should be considered when evaluating industrial equipment.
Clamping Force
Clamping force keeps the die closed during metal injection. It must be sufficient to counteract the internal pressure generated during filling.
Machines are available across a wide range of clamping capacities for different component sizes and casting requirements.
Shot Capacity
Shot capacity indicates the quantity of molten metal the injection system can handle during a casting cycle.
The required capacity depends on the component weight plus the runner, gate, and overflow system.
Injection Pressure
Injection pressure affects cavity filling, surface detail, and casting characteristics. The required pressure depends on alloy, component geometry, wall thickness, and process design.
Injection Speed
Injection speed controls how quickly molten metal enters the die cavity. High-speed injection is commonly associated with high pressure die casting.
Die Size
The machine must accommodate the required die dimensions and allow adequate space for mounting, ejection, cooling, and maintenance.
Cycle Time
Cycle time includes die closing, injection, solidification, opening, ejection, and associated operations. Shorter and consistent cycles can improve production throughput when appropriate for the casting.
Materials Used in Die Casting
Aluminum, zinc, magnesium, and selected copper-based alloys are among the materials used in die casting.
Aluminum
Aluminum alloys provide a combination of low density, strength, corrosion resistance, and castability. They are widely used in automotive, industrial, electrical, and consumer components.
Zinc
Zinc alloys can provide good dimensional accuracy and surface characteristics. Hot chamber die casting is commonly associated with zinc alloy production.
Magnesium
Magnesium is lightweight and can be used where reducing component mass is important. Processing requires appropriate equipment, alloy handling, and safety controls.
Copper-Based Alloys
Certain copper-based alloys can be die cast, although their higher processing temperatures can impose greater demands on machine components and dies.
Applications of Industrial Die Casting Machines
Die casting equipment is used across numerous manufacturing sectors.
Automotive Components
Common applications include:
- Transmission housings
- Motor housings
- Structural brackets
- Pump components
- Gear housings
- Automotive covers
- Electronic housings
Electrical and Electronics
Die casting can produce housings, connectors, heat-management components, brackets, and other metal parts requiring repeatable dimensions.
Industrial Machinery
Applications include pump bodies, motor housings, gearbox components, machine brackets, and equipment enclosures.
Consumer Products
Die casting is used for hardware, appliance components, handles, housings, fittings, and decorative metal parts.
Renewable Energy Equipment
Aluminum and other cast components can be incorporated into equipment housings, structural components, electrical assemblies, and thermal-management systems.
High Pressure Die Casting Process
High pressure die casting is commonly divided into controlled process stages.
Clamping
The machine closes and locks the die under the required clamping force.
Injection
A controlled shot of molten metal is injected into the cavity through the runner and gate system.
Pressure Intensification
Pressure is maintained during solidification to help compensate for shrinkage and support cavity filling.
Cooling
The casting remains in the die until sufficient solidification has occurred.
Ejection
The die opens and ejector mechanisms remove the casting.
Trimming
Flash, gates, runners, and other excess material are removed before further processing.
Automation in Die Casting
Automation has become an important part of modern die casting production.
Automated systems can support:
- Molten metal transfer
- Die spraying
- Part extraction
- Trimming
- Machine loading
- Machine unloading
- Vision inspection
- Dimensional inspection
- Data collection
Robotic extraction systems can remove castings from the machine while reducing manual handling around hot components.
Process monitoring can also record injection pressure, velocity, die temperature, cycle time, and other parameters.
Quality Control in Die Casting
Quality control helps identify defects and maintain dimensional consistency.
Common Casting Defects
Manufacturers may monitor for:
- Porosity
- Cold shuts
- Misruns
- Flash
- Cracks
- Inclusions
- Shrinkage
- Surface defects
- Dimensional deviations
Inspection Methods
Quality programs can include:
- Visual inspection
- Dimensional measurement
- X-ray or radiographic inspection
- Leak testing
- Hardness testing
- Metallurgical analysis
- Coordinate measuring machine inspection
The appropriate inspection method depends on the component's function and quality requirements.
Factors Affecting Die Casting Quality
Metal Temperature
The molten metal must remain within the appropriate processing range. Temperature variation can affect fluidity and solidification behavior.
Die Temperature
Controlled die temperature helps maintain consistent filling and solidification conditions.
Injection Parameters
Injection speed, pressure, acceleration, and intensification influence how the cavity fills.
Die Design
Runner dimensions, gates, vents, cooling channels, and cavity geometry all influence casting quality.
Lubrication and Release Agents
Appropriate die-release systems help prevent sticking and support consistent part removal.
Cooling Rate
Uneven cooling can contribute to distortion, residual stresses, and dimensional variation.
Maintenance of Industrial Die Casting Machines
Regular maintenance supports stable machine performance and reduces mechanical problems.
Important maintenance activities include:
- Inspecting hydraulic systems
- Checking hydraulic fluid condition
- Cleaning die surfaces
- Inspecting ejector mechanisms
- Checking injection components
- Inspecting clamps and tie bars
- Cleaning filters
- Checking cooling circuits
- Inspecting electrical connections
- Calibrating sensors
- Monitoring abnormal vibration or noise
Die maintenance is equally important because worn or damaged cavity surfaces can affect casting dimensions and surface quality.
How to Select Industrial Die Casting Machines
Machine selection should begin with the casting requirements rather than machine size alone.
Consider:
- Alloy type
- Component dimensions
- Component weight
- Required clamping force
- Shot capacity
- Injection pressure
- Injection speed
- Die dimensions
- Cycle requirements
- Automation requirements
- Quality-control requirements
- Available floor space
- Utility requirements
- Maintenance capabilities
For high-volume production, automation and process monitoring may become particularly important.
Frequently Asked Questions
What are industrial die casting machines used for?
They are used to produce metal components by injecting molten non-ferrous alloys into reusable dies under controlled pressure. Applications include automotive, electronics, machinery, electrical equipment, and consumer products.
What is the difference between hot chamber and cold chamber die casting?
Hot chamber systems keep the injection mechanism closely associated with the molten metal, while cold chamber systems use a separate furnace and transfer molten metal into the injection chamber for each cycle.
Which metals are commonly used in die casting?
Aluminum, zinc, magnesium, and selected copper-based alloys are commonly processed through different die casting technologies.
What is clamping force in a die casting machine?
Clamping force is the force used to keep the die halves closed during injection. Adequate force helps prevent die separation and excessive flash.
How can die casting quality be improved?
Quality can be improved through accurate alloy-temperature control, appropriate die design, controlled injection parameters, effective cooling, proper die maintenance, and systematic inspection.
Conclusion
Industrial die casting machines provide a highly controlled method for producing complex metal components with repeatable dimensions and surface characteristics. Hot chamber, cold chamber, high pressure, and low pressure technologies each address different material and production requirements.
Machine performance depends on coordinated control of clamping force, injection pressure, speed, die temperature, alloy temperature, cooling, and ejection. Automation and digital monitoring can further improve process consistency and production visibility.
A suitable die casting system should therefore be selected according to the alloy, component geometry, production requirements, quality specifications, and long-term operating conditions.